Quick Performance Matrix
Capacity Range:
100 Liters to 10,000 Liters
MOC Options:
SS316, SS304, MS (Mild Steel)
Motor Drive:
Full Vacuum Rated (-760 mmHg / -1 Bar) with Reinforced Dished Ends
Output Fineness:
100% Helium Leak / Hydrostatic Vacuum Retaining Tested
Origin / Plant:
Vatva GIDC, Ahmedabad, India
Engineering Overview & Design Highlights
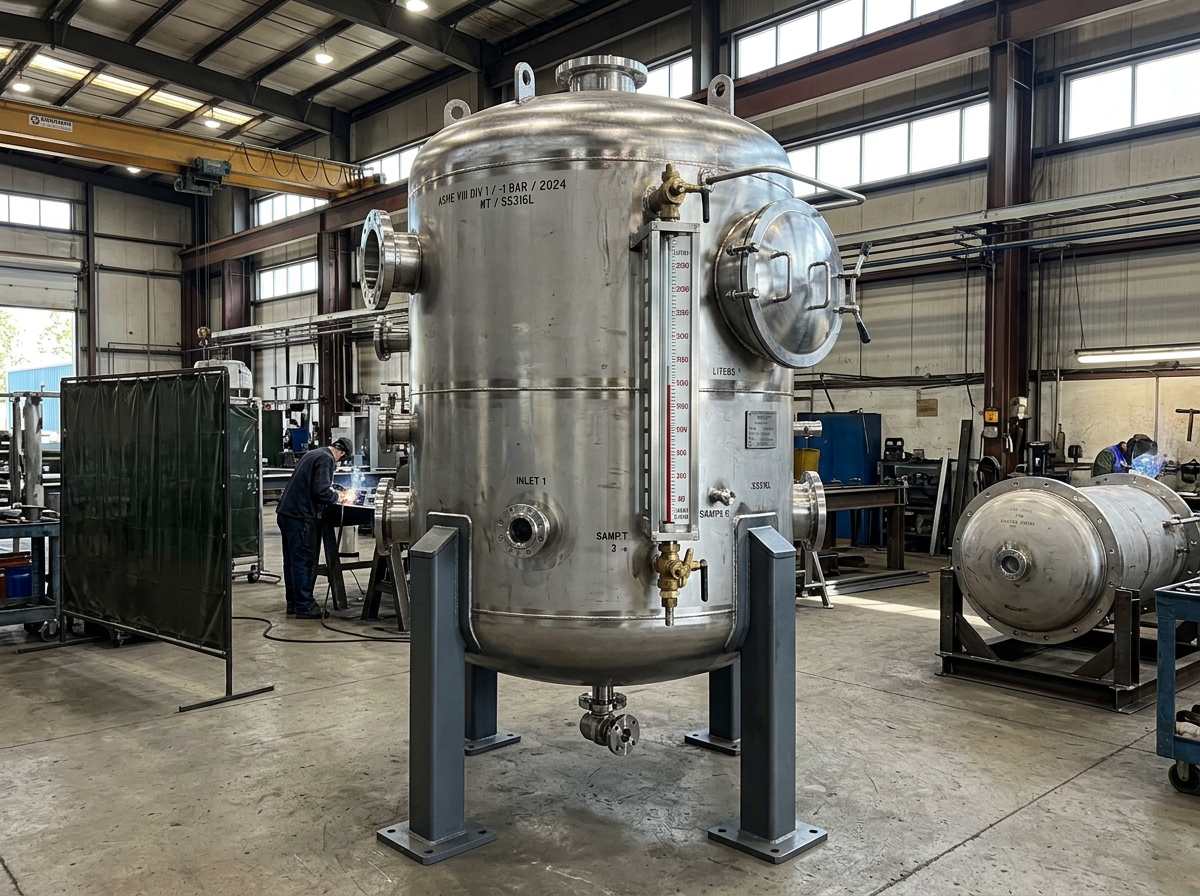
The JMEF Vacuum Receiver Tank (Distillate Accumulator) is designed to safely accumulate, separate, and measure distilled liquid solvents exiting overhead condensers under deep vacuum. Built in Vatva GIDC, Ahmedabad, these vessels eliminate the need to break vacuum on the primary reactor during continuous or semi-batch distillation cycles.
Working Principle & Mechanical Operation
Vapor condensed by the overhead condenser flows by gravity into the vacuum receiver vessel maintained under identical negative pressure. Once filled, the receiver is isolated via vacuum-rated ball valves, equalized with atmospheric pressure or nitrogen, and drained into storage without disturbing reactor vacuum.
Salient Features & Technical Advantages
-
Heavy-wall construction engineered to prevent vessel implosion under severe full vacuum (-760 mmHg).
-
Borosilicate tubular level gauge or reflex sight glass for precise real-time liquid volume monitoring.
-
Multiple flanged inlet ports for condensate inlet, vacuum balancing, nitrogen blanketing, and vent.
-
Dual-receiver twin system available for continuous uninterrupted distillation discharge.
-
Sanitary mirror-polished interior with dished ends ensuring zero product retention upon draining.
Comprehensive Technical Specifications
| Technical Parameter |
Standard Engineering Specification |
| Capacity |
100 L to 10,000 L |
| Operating Pressure |
Full Vacuum (-1 Bar) to 3 Bar positive pressure |
| Design Standards |
ASME Section VIII Div 1 & IS 2825 Codes |
| Level Gauge |
Borosilicate Glass Tube with SS protective guard & auto-shutoff valves |
| Connection Ports |
Condensate inlet, vacuum line, vent, drain, nitrogen purge, high-level sensor |
| Mounting |
Sturdy 4-leg support frame with leveling pads or floor mounting base |
| Manufacturing Plant |
Phase-1, Vatva GIDC, Ahmedabad, Gujarat, India |
| Compliance Standards |
ASME Section VIII Div 1, IS 2825 & cGMP Sanitary Standards |
| Export Packaging |
ISPM-15 Fumigated Seaworthy Wooden Box with Rust-Preventive VCI Wrapping |
| Dispatch Location |
Vatva GIDC, Ahmedabad, Gujarat, India (Direct Domestic & Global Dispatch) |
| International Trade Terms |
FOB, CIF, CFR, Ex-Works & Letter of Credit (LC / TT) |
Industrial Applications
Solvent Recovery Systems: Collecting acetone, toluene, methanol, IPA from condensers.
Pharma & APIs: Sterile collection of distillate fractions during vacuum drying & rotary evaporation.
Resin & Chemical Plants: Condensate receivers, knock-out pots, and liquid seal drums.
Frequently Asked Questions About Vacuum Receiver & Solvent Trap Tank
Can we discharge distillate without breaking reactor vacuum?
Yes, with our twin-receiver arrangement, while Receiver A is collecting condensate under vacuum, Receiver B can be isolated and pumped out to storage without disturbing reactor vacuum.
Direct Factory Price
Request a Quote for Vacuum Receiver & Solvent Trap Tank
Get direct manufacturer pricing from our Vatva GIDC, Ahmedabad engineering plant.
Related Process Machinery